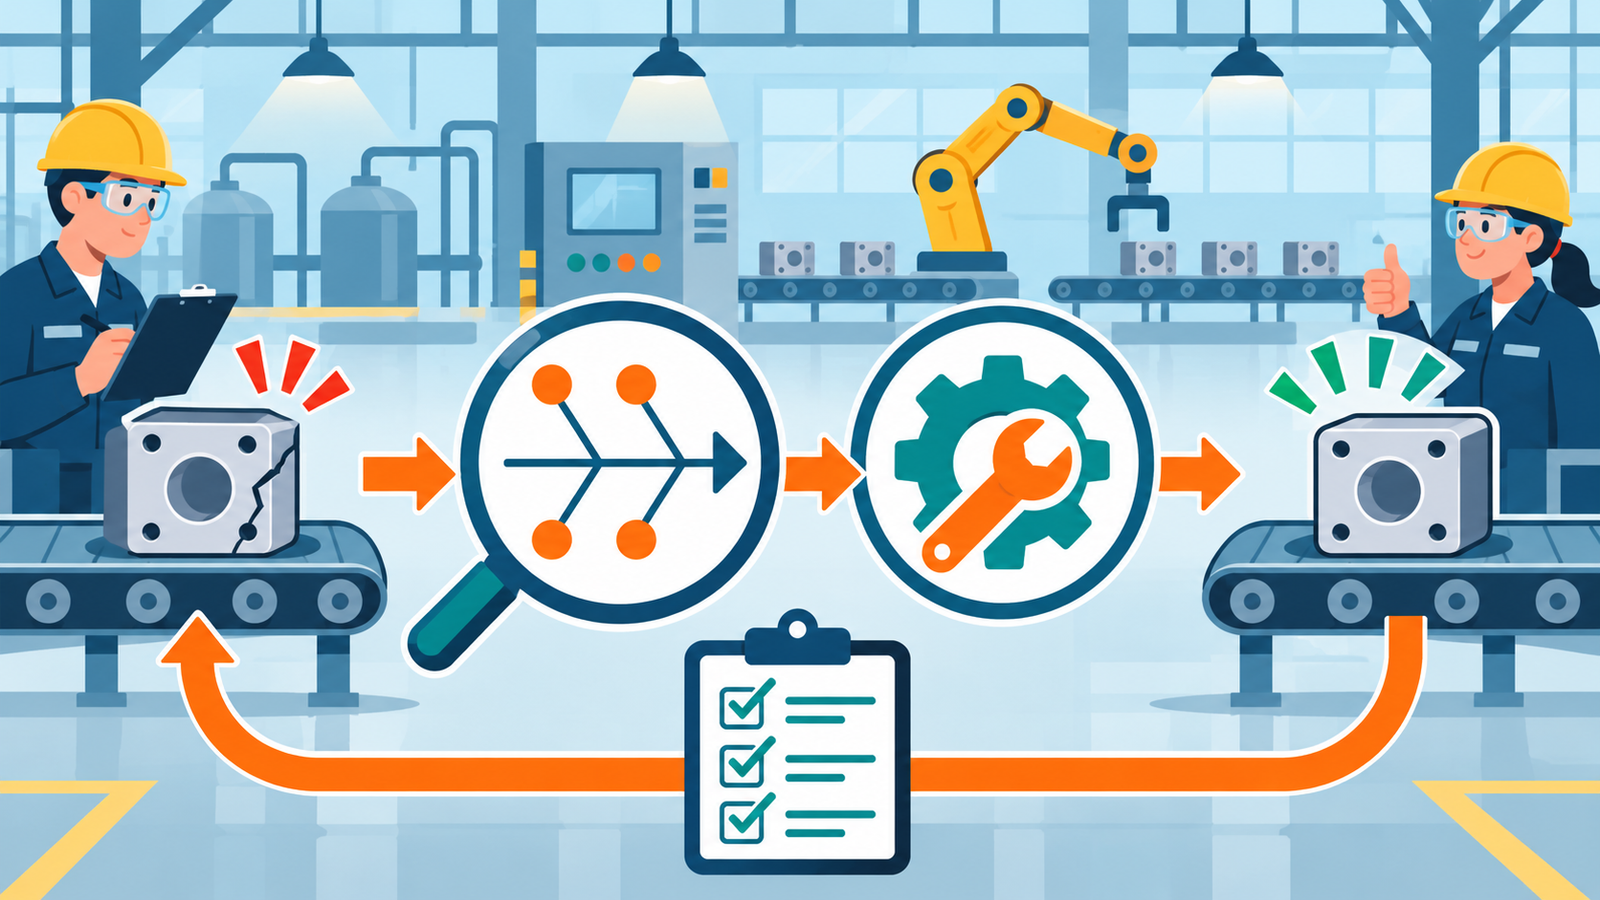
Every supplier can fix a bad batch. The test is whether the same defect appears on the next order. A corrective action plan is how you move a factory from apologising for a problem to removing its cause, and how you check that it did.
What is a CAPA? CAPA stands for corrective and preventive action. A corrective action removes the root cause of a problem that has already occurred so that it does not recur; a preventive action removes the cause of a potential problem before it occurs. A supplier CAPA documents the problem, its root cause, the actions taken and the proof they worked.
This guide covers when to ask for one, a six-step process, root-cause methods such as 5 Whys and 8D, how to judge a supplier’s answer, and how to verify the fix. For the immediate decision about a batch that has just failed (rework, sort, re-inspect or refuse), see what to do when a shipment fails inspection; CAPA is what comes after that decision.
Correction, corrective action and preventive action
These three terms are often mixed up, and suppliers sometimes offer the first while calling it the second.
| Term | What it does | Example (stitching failure on a bag strap) |
|---|---|---|
| Correction (containment) | Deals with the affected goods now | Sort and re-stitch all straps in the current order |
| Corrective action | Removes the cause of the problem that happened | Replace the worn sewing-machine part and set a thread-tension check at the start of each shift |
| Preventive action | Removes the cause of a problem that could happen elsewhere | Add the same tension check to all sewing lines and to the maintenance schedule |
A rework is a correction, not a corrective action. If a supplier’s "corrective action plan" only describes how the current goods were fixed, it is incomplete. Note that the ISO 9001 quality-management standard in its 2015 edition handles prevention mainly through risk-based thinking rather than a separate preventive-action clause, but buyers and suppliers still widely use the CAPA label.
When should you ask a supplier for a corrective action plan?
Ask for a formal plan when:
- an inspection fails, especially for major or critical defects (see how critical, major and minor defects are classified);
- the same defect type appears on two or more orders, even if each passed AQL;
- a customer complaint or return pattern points to a manufacturing cause;
- a factory audit finds a system weakness, such as no incoming material checks;
- a supplier changed a material or process without approval.
For small one-off cosmetic issues, a short written explanation may be enough. Match the effort to the risk.
The six-step CAPA process
- Define the problem with evidence. State what was found, where, how many units, against which requirement. Attach the inspection report, photos and the relevant line of your specification.
- Contain it. Agree immediate actions to protect the current order and any stock or work in progress: sorting, rework, holding suspect material, checking other orders using the same components.
- Find the root cause. Ask why the defect occurred and why it was not detected, using a structured method such as 5 Whys or a cause-and-effect (fishbone) diagram.
- Plan and implement corrective actions. Actions that remove the root cause, each with an owner and a completion date: a process change, tool repair, new fixture, revised work instruction, supplier change for a component.
- Extend to preventive actions. Apply the fix to similar products, lines or processes where the same cause could occur, and update the documents that control them.
- Verify effectiveness and close. Confirm with evidence and with results on following production that the problem has not recurred, then close the CAPA.
Root-cause methods: 5 Whys, fishbone and 8D
5 Whys
The 5 Whys method, associated with the Toyota Production System, asks "why?" repeatedly until it reaches a cause that can be acted on. Five is a guide, not a rule.
Hypothetical example: straps detaching from backpacks.
- Why did straps detach? The stitching broke under load.
- Why did the stitching break? Stitch density was lower than specified.
- Why was stitch density low? The machine’s stitch-length setting had drifted.
- Why did it drift unnoticed? No one checked settings at the start of shifts.
- Why was there no check? The work instruction did not include it.
The actionable root cause is the missing set-up check, not "worker carelessness". Good root-cause analysis also asks a second chain of questions: why did the factory’s own QC not catch it? A detection failure needs its own corrective action.
Fishbone (Ishikawa) diagram
A fishbone diagram groups possible causes under headings such as man (people), machine, method, material, measurement and environment. It is useful when a problem has several possible causes and the team needs to rule them out systematically before applying 5 Whys to the likely ones.
8D problem solving
8D (Eight Disciplines) is a structured problem-solving report widely used in manufacturing, particularly in automotive supply chains where it originated, and described in quality-body references such as those from ASQ (the American Society for Quality). It typically covers: forming a team; describing the problem; interim containment; root cause; choosing and verifying permanent corrective actions; implementing and validating them; preventing recurrence; and recognising the team. Many larger Chinese factories are familiar with 8D reports. For smaller workshops, a simpler CAPA form covering the six steps above is often more realistic than insisting on a full 8D.
What a supplier’s corrective action plan should include
| Element | A credible answer | A weak answer |
|---|---|---|
| Problem description | Specific defect, quantity, order, requirement breached, evidence | "Some quality problems" |
| Containment | What was done to the current order and other stock, with numbers | "All goods checked" |
| Root cause (occurrence) | A specific process, machine, material or method cause | "Worker was careless" |
| Root cause (detection) | Why in-line or final QC missed it | Not mentioned |
| Corrective actions | Concrete changes, each with owner and date | "We will pay more attention" |
| Preventive actions | Where else the cause could apply and what was changed there | Not mentioned |
| Updated documents | Revised work instructions, checklists, control plans | None |
| Evidence | Photos, new checklist forms, training records, test results | Promises only |
| Verification plan | How and when effectiveness will be confirmed | Not mentioned |
Red flags in a CAPA response
- The root cause is always "operator error", and the only action is "retrained the worker". Training can be part of a fix, but on its own it rarely prevents recurrence.
- Every action is due "immediately" with no owner.
- The plan arrives before the investigation could realistically have been done.
- The same CAPA wording appears for different problems.
- The supplier blames the specification but never asked for clarification. If the specification really was ambiguous, fix it: our guide to writing a quality specification factories can follow helps.
How to request a CAPA from a Chinese supplier
Make it easy to answer well:
- Send a short template with the six steps as headings, in English and Chinese if possible.
- Attach the evidence: the inspection report, defect photos and the relevant specification lines or golden sample reference.
- Set a realistic deadline: a quick containment answer, then a fuller root-cause response once the factory has investigated.
- Ask for a named owner at the factory, ideally the QC manager or production manager rather than the salesperson.
- Keep the tone factual. The aim is a fix, not blame. Factories respond better to a clear process than to anger.
A planned guide to communicating custom requirements to Chinese suppliers covers wider communication practices.
How do you check that a corrective action worked?
A CAPA is only as good as its verification. Practical checks:
- Evidence of implementation. Photos or video of the changed process, new fixture or updated work instruction, and records showing it is used.
- On-site confirmation. For serious or repeated problems, have someone visit the line to see the change in place. A focused re-audit can be scoped from our factory audit checklist.
- Check early in the next order. Book a during-production inspection so the specific defect is checked while production can still be adjusted.
- Tighter final inspection for a period. Pay special attention to the defect type at the next final inspections, and consider stricter sampling for the affected class. How sampling levels and AQL limits work is explained separately.
- Track the trend. Record defect rates for that defect type across orders. Close the CAPA only after an agreed number of consecutive lots show no recurrence.
- Watch customer feedback. Returns and complaints after delivery are the final test.
If verification shows the problem has returned, re-open the CAPA and look again at the root cause; the first one identified was probably a symptom.
When corrective action is not enough
Sometimes the honest conclusion is that the supplier cannot or will not fix the problem: the root cause is a lack of equipment, skills or management commitment. Signs include repeated recurrence after closed CAPAs, refusal to share evidence, or a factory that is simply too small for your requirements. At that point, consider a formal factory audit to assess capability, or start qualifying an alternative supplier before the next order.
Building CAPA into production follow-up
CAPA works best when it is part of a routine rather than a reaction. Keep a simple log of open and closed corrective actions per supplier, review it before each new order, and link it to your production follow-up so that milestones include checking open actions. Our upcoming guide on production follow-up with Chinese factories covers how to set those milestones. Buyers in Bangladesh, who are rarely able to visit factories at short notice, benefit particularly from having this evidence collected on the ground in China.
Getting help with supplier corrective action
Jingxin Sourcing carries out product inspections and physical factory audits in Yiwu, Shenzhen and Guangzhou, which are the checks that both trigger and verify corrective action. You can read how inspections are organised on our quality-control service page, or see how on-site supplier assessments work under China factory audits. For how corrective action fits into the full sequence of quality checks, see our guide to inspection stages when sourcing from China. If you are deciding who should do these checks, our comparison of independent inspectors and sourcing-company QC sets out the trade-offs.
Frequently Asked Questions
Closing note
A good corrective action plan reads like an engineering record, not an apology: a specific cause, specific changes, named owners, dates and evidence. Ask for that standard every time, verify it on the next order, and the number of problems worth writing CAPAs about tends to fall.